Description
Overview
Type: PVC tarpaulin coating line, knife (doctor blade) coating with a double-sided vertical coating head, 2 horizontal precision coating heads and a surface treating (lacquer) machine
Condition: New, built to order
Fabric width: 4,000 mm (157.5 in)
Machine width: 4,200 mm (165.4 in)
Line speed: 4 to 40 m/min (13 to 131 ft/min)
Working temperature: 120 C to 220 C (248 F to 428 F)
Installed capacity: 370 kW, plus 80 kW electric heating per group on 3 groups
Compressed air supply: 0.5 MPa (73 psi)
Burner inlet pressure regulator valve working pressure: 0.05 MPa (50 kPa)
Cloth inlet and cloth outlet: open width rolling
Control panel position: left hand or right hand
Suitable for coating luggage fabric, tarpaulin fabric and industrial fabric with PU, PVC, AC, rubber and water-based glue
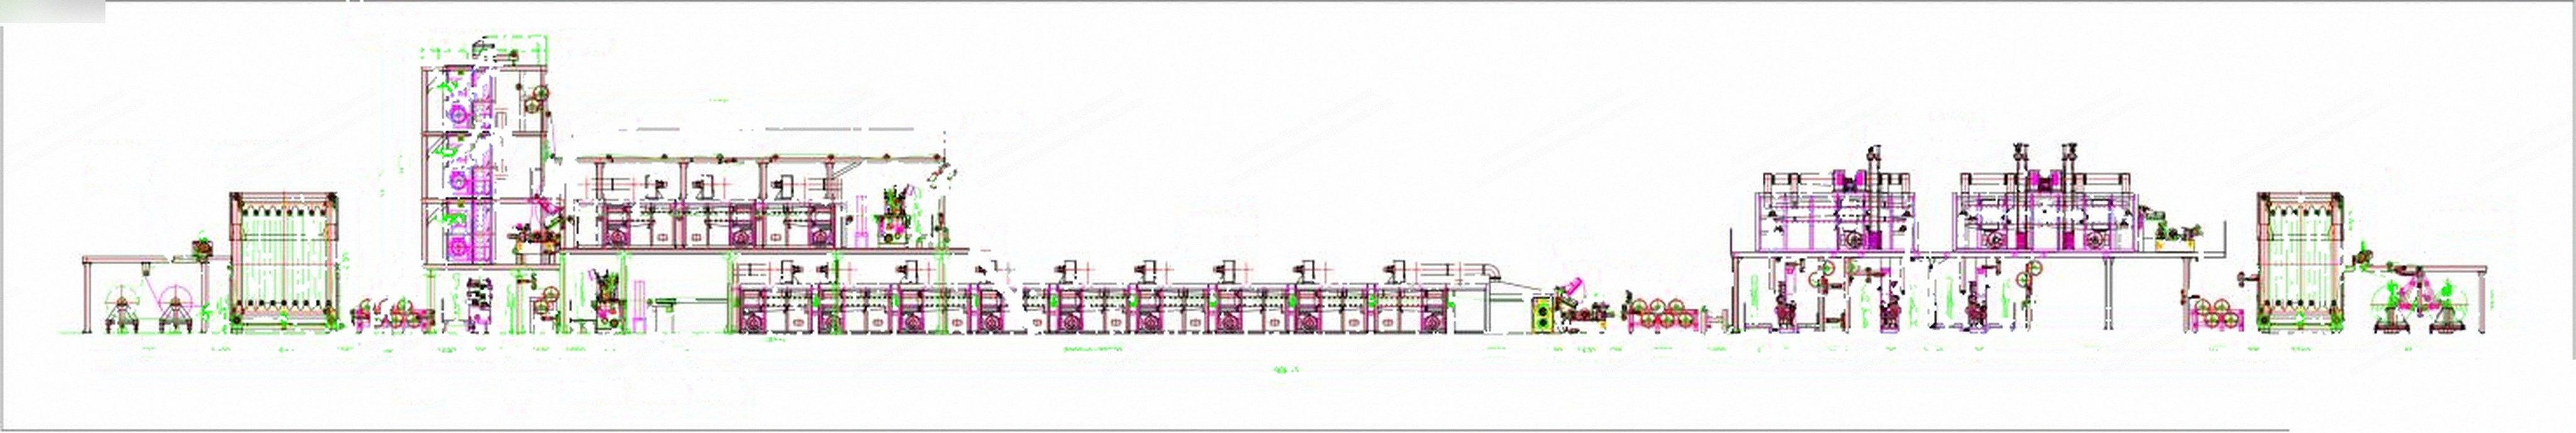
Process Flow
Double station unwinder
Fabric feeding frame with sewing device
60 m (196.9 ft) accumulator
6-roller ironing device
Double-sided vertical coating table
7.5 m (24.6 ft) vertical oven
2-roller cooling device
Traction device
Horizontal precision coating table with thickness gauge
9 m (29.5 ft) hot air oven, guide roller type
Calander device, then 2-roller cooling device
Second horizontal precision coating table with thickness gauge
Main hot air stenter oven
IR heating device, calander device, 6-roller cooling device
Surface treating machine, then IR heating device and calander device
4-roller cooling device
45 m (147.6 ft) accumulator
Edge cutting device and fabric outing device
Double-station active winder with A-frames
Coating Heads
Double-sided vertical coating head: wallboards welded from 25 mm steel plate, under frame of 16 channel steel, tension control, manual incline adjustment, 4 blade coating units placed on both sides of the fabric, 2 stainless steel material tanks that turn manually and move front and back, 300 mm (11.8 in) braking roller with pneumatic braking, 304 stainless steel receiver tank
Horizontal precision coating tables: 2 sets, each fitted with a PVC special coating table and a 420 mm (16.5 in) coating roller
Coating blade: segmented adjustable knife holder, manual straightness adjustment, electric angle adjustment with locking structure, knife shoulder frame on linear bearing slide rails
Blade lifting: cylinder driven with servo motor fine adjustment, 2 sets left and right
Blade fore and aft adjustment: servo electric on linear bearing slide rails, 2 sets left and right
Also on each head: cloth-out height adjusting guide roller with blade change device, manually lifted cleaning tank, water holding device, left and right damming device, 2 edge correction devices, 2 guide rollers, magnetic powder tension control roller, pneumatic feeding pump and thickness gauge
Ovens and Heating
Vertical oven: 7.5 m (24.6 ft) in 3 chambers of 2.5 m (8.2 ft), frame of 12 shape steel
First horizontal oven: 9 m (29.5 ft) in 3 chambers of 3 m (9.8 ft), guide roller type, gas burner per chamber, 2 circulating fans per section with inverted conical nozzles and adjusting dampers, Teflon-covered 190 mm (7.5 in) supporting wheels, P.I.D electronic temperature control
Main stenter oven: the process flow lists 28 m (91.9 ft); the component list and the oven description give 21 m (68.9 ft) in 7 chambers of 3 m (9.8 ft). Confirm the final length with the seller
Stenter oven detail: cast iron rail with lower supporting mode, entry end box of steel sheet with thick steel H frame track, IR edge detector pair with motorised actuator, 2 pairs of clipping devices, 8 width adjustment units each with a 0.55 kW drive and one electronic control per chamber, one pair of large area heat exchange heating devices per chamber regulated by a 3-way oil control valve, 2 energy-saving fans per chamber on 7.5 kW high temperature inverter drives, moisture exhaust with an air door per opening
Surface treatment ovens: 1 oven of 5.5 m (18.0 ft) and 1 oven of 6.5 m (21.3 ft), heat transfer oil regulated through a temperature control module, frequency driven fans with pull-out filters, Teflon coated active guide roller, top exhaust with dampers
Oven insulation on the vertical oven, the first horizontal oven and the stenter oven: 150 mm (5.9 in) top panel and 120 mm (4.7 in) side panel, 1.2 mm cold rolled steel outer sheet, galvanized inner forming, rock wool insulation, sealed entry chamber with a rail-mounted seal plate. On the 2 surface treatment ovens the insulating panel and the top panel are both 120 mm (4.7 in), with sealing elements at the panel to frame junctions
Each chamber has its own temperature probe, controller and display, and its own exhaust device with an adjustable air door
Handling, Cooling and Finishing
Unwinding: double station centering unwinder with magnetic powder brake, 2 sets
Fabric feeding: frame of Q235-A steel plate with external reinforcing plates, 2 guide rollers, fabric tightening device, sewing device with fabric pressure device, cross transfer device and sewing machine
Accumulators: 45 m (147.6 ft) and 60 m (196.9 ft), opposite open type, chain connected with rack synchronization, storage and fabric tension set by cylinder pressure, top and bottom guide rollers 190 mm (7.5 in) diameter
6-roller ironing device: 4 heated turning rollers and 2 cold water rollers, all 520 mm (20.5 in) diameter, with gear drive, tension control and mold temperature control
Cooling devices: 2 two-roller devices, each with 520 mm (20.5 in) jacketed cold water rollers on a 4 kW R series reducer motor, plus 1 six-roller device and 1 four-roller device with 520 mm (20.5 in) active rollers on 5.5 kW reducer motors
Calander devices: 3 sets, wallboards of 40 mm steel plate, 450 mm (17.7 in) active rubber-covered squeezing roller on an 11 kW reducer with double row cylindrical roller bearings, 450 mm (17.7 in) steel mirror passive roller, both-side oil cylinder pressure of not less than 10 t rising to not less than 20 t after squeezing, hydraulic system and pressure sensor
IR heating devices: 2 sets, stainless steel reflector plates, 6 groups of black IR heating tubes, cylinder lifting
Edge cutting: 5 straight knives with 5 knife position adjusters, guide roller and 2 edge winder devices
Traction: 400 mm (15.7 in) rubber traction roller with reducer motor
Winding: double station big package winder, C-section steel frame, 270 mm (10.6 in) rubber cloth-out roller on aligning bearings, hydraulic pressure arm, 2 transitional guide rollers, hand wheel adjusted bending roller, electrostatic eliminator, 2 center winders with 11 kW reducer motors, vector converter constant tension and 1,200 mm (47.2 in) maximum roll diameter, 5 A-frames on universal wheels
Working platform: 250H steel columns, 200H section steel, 12.6 channel and I-beam with patterned walkway plate, 1 in steel pipe barriers and ladders
Controls
Frequency converters and PLC for stepless regulation, with synchronous control between units by angle sensor regulation
Suspended platform on each coating head and a small platform at the cloth-out; fore and aft sections can run separately or on line
Control cabinet: upright welded steel, with ammeter, voltmeter, thermometer, no-fuse breaker, switches, terminal cable trough, internal wiring and cooling fan
Control board: motor start, run and stop, signal lamps, emergency shutdown, buzzer and motor tachometer
Named components: Mitsubishi touch screen, Yaskawa transmission and circulating fan inverters, Schneider contactors, relays, buttons, switches and indicator lights, AIRTAC main pneumatic components